Textile Machinery: Roller Gap and Dancer-Tension Position
Drafting and winding on textile machines use a displacement sensor, with fly and humidity the environmental focus. Displacement measurement on textile machinery concentrates on two places, drafting and loading and winding and tension. On the drafting side are roller gap and press-roller closing, which determine yarn linear density and fabric thickness. On the winding side are dancer (tension-arm) displacement and package diameter, which determine tension stability and package quality. The shared environment of both lines is airborne fly (short-fibre dust), high shop humidity, and oil at some stations, so dust protection and resistance to fibre wrapping of displacement measurement stand out.
Drafting side: roller gap and loading
In a roller-drafting system the top roller is loaded by the weighting arm onto the bottom roller; the gap between the two rollers determines fibre nipping and draft ratio. Displacement feedback is used for loading control, multi-spindle loading-consistency monitoring, and gap compensation after wear. Multi-spindle consistency is the key point — if gaps differ among spindles on the same machine, count variation results. Multi-channel sensors of the same model and the same measuring range are recommended, with attention paid to repeatability (typically of the order of ±0.002 mm; see the three accuracy terms) rather than the non-linearity figure of a single unit. If the loading actuator is a pneumatic or hydraulic cylinder, the selection framework is given in why hydraulic cylinder position control uses magnetostrictive sensing.
Winding side: dancer and package diameter
Dancer position reflects web/yarn tension directly. A displacement sensor reads the linear displacement corresponding to the dancer angle; the controller adjusts unwind or rewind speed accordingly to hold constant tension. Package diameter grows with winding; displacement feedback can be used for diameter tracking, forming a dual closed loop with the dancer. These mechanisms are mostly oscillating or short-stroke linear motion; a 5-20 μm resolution grade is recommended, and the refresh rate should be checked against the control cycle (see matching response time to the control cycle). After a power loss the dancer absolute position is retained, so homing on power-up is unnecessary (see absolute vs. incremental position).
Typical measuring-point layout on textile machinery
| Measuring point | Control objective | Recommended form | Resolution grade | Environmental focus |
|---|---|---|---|---|
| Roller / press-roller gap | Linear-density consistency | Profile type or pneumatic/hydraulic in-cylinder | 5-20 μm | Fly, oil |
| Dancer | Constant tension | Profile type (short stroke) | 5-10 μm | Fibre wrapping |
| Package-diameter tracking | Package quality | Profile type | 20-50 μm | High humidity |
| Warp-beam / cloth-beam positioning | Alignment and start/stop | Profile type | 10-20 μm | Vibration, dust |
Installation points in fly and high-humidity environments
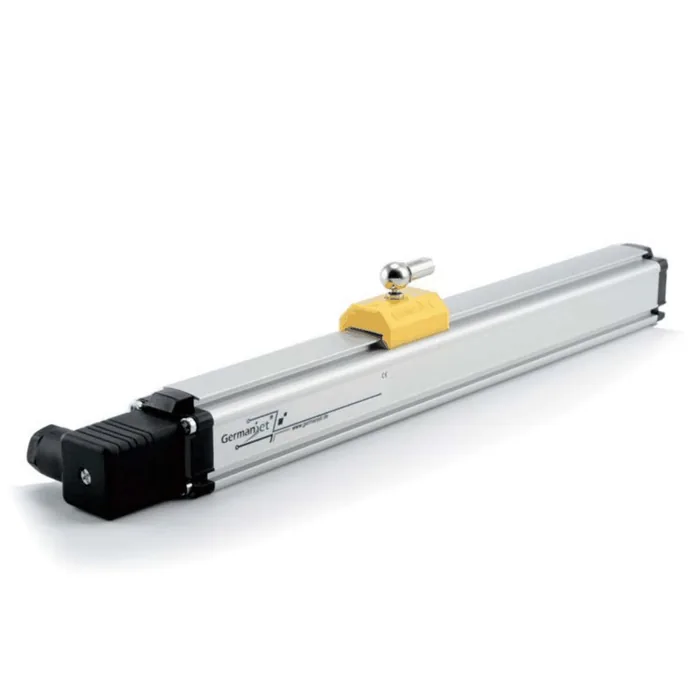
Fly wraps on the rod and magnet, changing the working gap over time and possibly being carried into the connector; high humidity tests the seal. Countermeasures: fit an anti-wrap sleeve or air-blow cleaning on the rod and specify IP67 or better connectors; wrapped fly shifts the working gap and drifts readings (for the meaning of each rating see IP protection ratings), and for profile-type products see Series 18 profile type. For wet areas or stations that require washdown, specify Series 13 mobile hydraulic. Installation and anti-loosening practice is in installing and commissioning in practice; troubleshooting of abnormal readings caused by fibre wrapping is in common-fault troubleshooting.
Interfaces and line integration
Textile equipment is typically built around a servo system. Position feedback may be SSI (deterministic timing, suited to the position loop; see Series 192 SSI digital interface) or a fieldbus type for centralised multi-axis management. Tight-cycle winding stations should check refresh rate and fieldbus synchronisation (see matching response time to the control cycle). Displacement schemes for industrial-robot peripheral axes can be compared with industrial robots: seventh-axis and vertical-axis position.
Practical tips for engineers
- IP65 means a 6.3 mm nozzle spraying water from any direction has no harmful effect; IP67 means no harmful ingress when immersed at 1 m depth.
- Contact-based sensors are typically only IP40 or IP50, whereas non-contact magnetostrictive transducers can reach IP65 or even IP67 — specify a non-contact type in high-dust, high-humidity environments.
Frequently Asked Questions
Q: What does roller gap affect?
It determines fibre nipping and draft ratio; multi-spindle consistency determines evenness of count. Repeatability of ±0.002 mm is used as the safeguard.
Q: How is dancer displacement used?
Dancer position reflects tension; displacement feedback adjusts speed to hold constant tension. It can form a dual closed loop with package diameter.
Q: How is fly wrapping protected against?
Fit an anti-wrap sleeve or air-blow cleaning, and use IP67 or better connectors. Specify Series 18 for profile mounting.
Related Products
Related Applications
Multi-Industry Application Cases for Magnetostrictive Displacement Sensors
View Details
Series 17 Hydraulic Cylinder Integrated Magnetostrictive Displacement Sensor Application Cases
View Details
Series 18 Profile Magnetostrictive Displacement Sensor Application Cases
View Details